Valve & Pump Components
Stainless Steel Valve Casting OEM:
China Factory — Zero-Porosity Guaranteed.
ISO 9001 Certified Foundry specializing in Silica Sol Investment Casting. We deliver zero-porosity components with superior internal surface smoothness, ensuring long-term performance in corrosive and high-pressure environments.
Technical Superiority
Our OEM Capabilities
Process
- Zero-Porosity Guarantee: Advanced degassing and silica sol techniques to eliminate internal defects and leak paths
- Dimensional tolerance: CT4–CT6 per ISO 8062 (as-cast)
- Weight range: 0.05 kg – 50 kg per piece
- Surface roughness: Ra 3.2–6.3 μm (as-cast); Ra 0.8–1.6 μm (machined)
Specialized Alloys
- 304, 316, 316L — general corrosion resistance for standard media
- 17-4PH — high-strength, precipitation-hardened for demanding applications
- Duplex 2205 / 2507 — expert casting for chloride and chemical resistance
- CF8M / CF3M — ASTM A351 pressure-retaining castings
Quality Assurance
- 100% Hydrostatic Pressure Testing for all valve & pump parts
- Spectrometer Material Analysis on every heat — full traceability
- CMM Dimensional Inspection with full inspection report
- EN 10204 3.1 Mill Test Certificate (standard, not an upgrade)
Technical Capabilities
Built for Pressure-Critical Applications
Zero Porosity. Pressure-Tested.
Silica sol process eliminates the macro-porosity common in sand casting. Every valve body and pump casing undergoes 100% hydrostatic pressure testing before shipment. X-Ray inspection available for critical applications.
Full Material Traceability
OES Spectrometer verification on every heat. EN 10204 3.1 Mill Test Certificates issued as standard — not as an upgrade. Your quality team will have the documentation they need on day one.
Casting + Machining. One Supplier.
We machine valve seats, bores, flanges, and threaded connections in-house with 4/5-axis CNC centers to ±0.01mm. No inter-supplier handoffs. No dimensional surprises when the cast part reaches the machine shop.
Products
Valve & Fluid Control Components
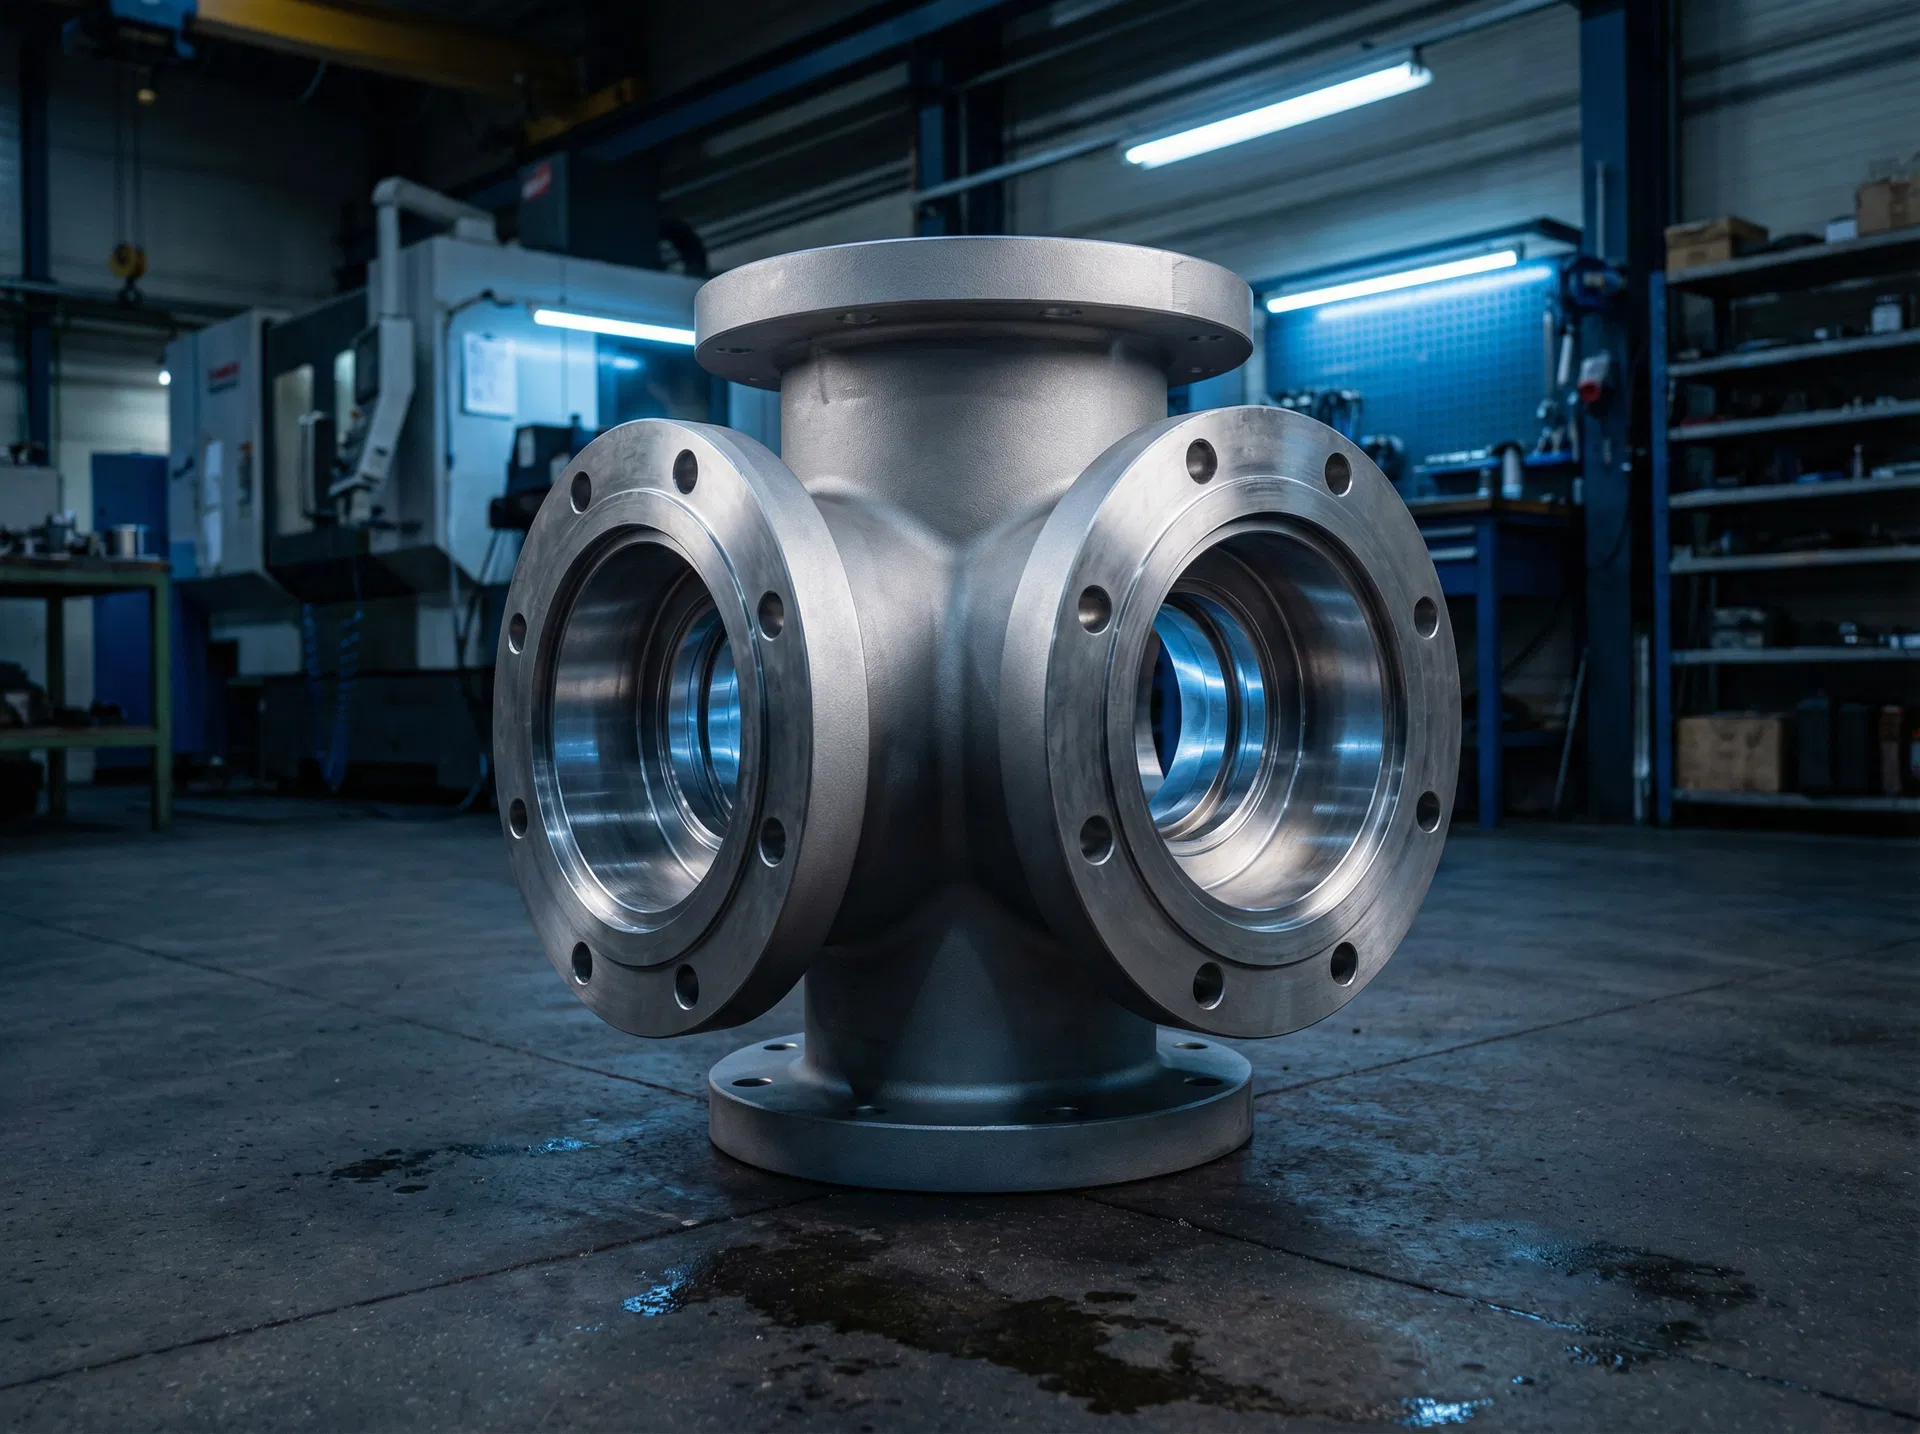
Valve Bodies (Gate, Ball, Check, Globe)
100% hydrostatic pressure test. 3.1 MTC standard.
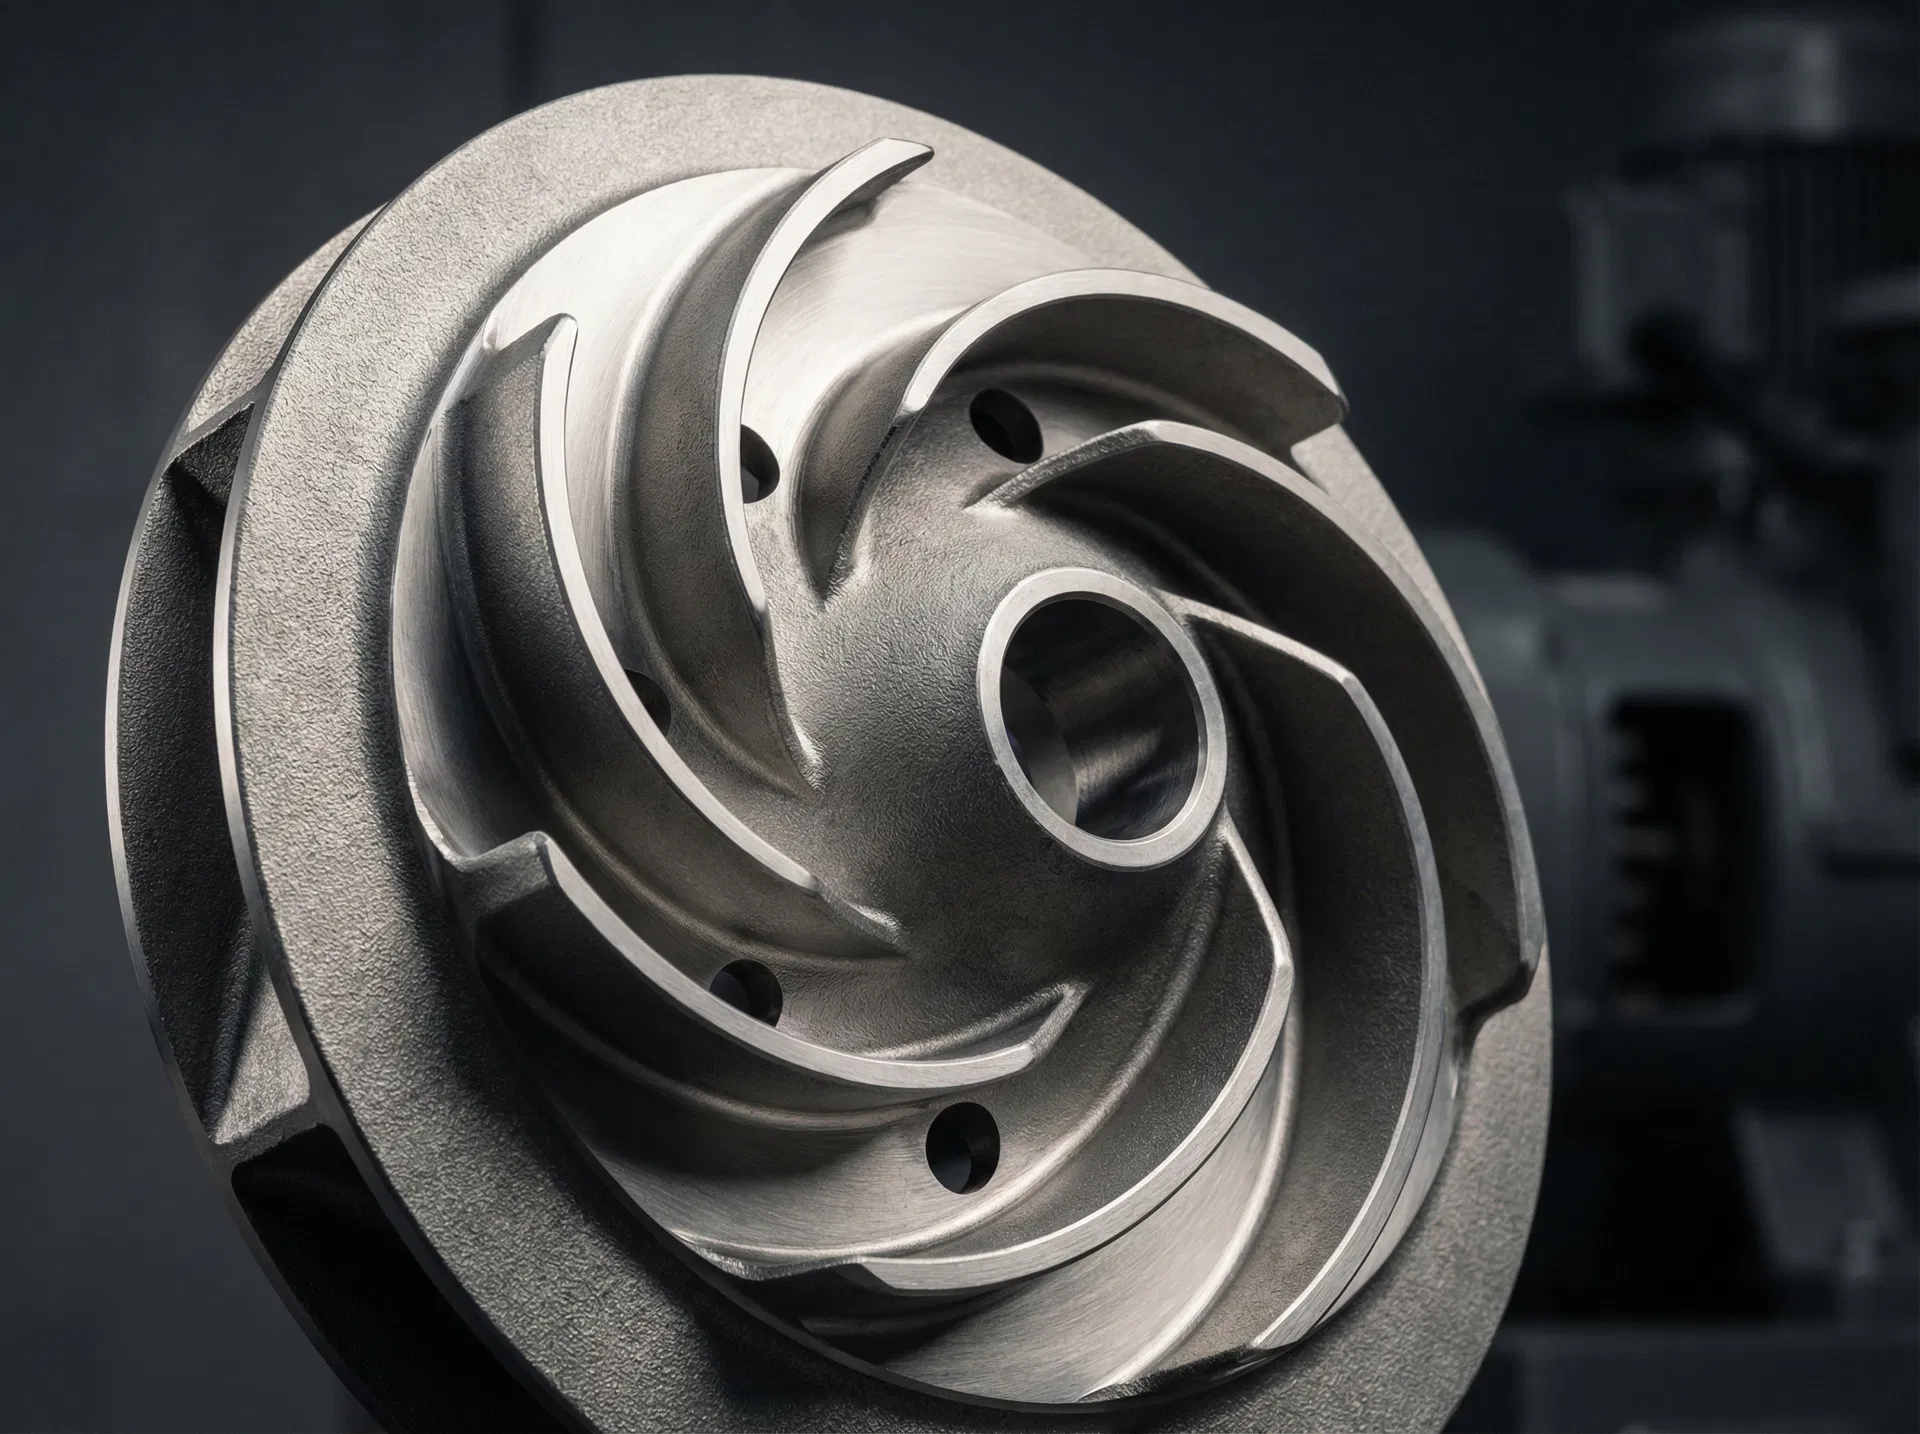
Pump Impellers
Dynamic balancing available. CMM inspection report.
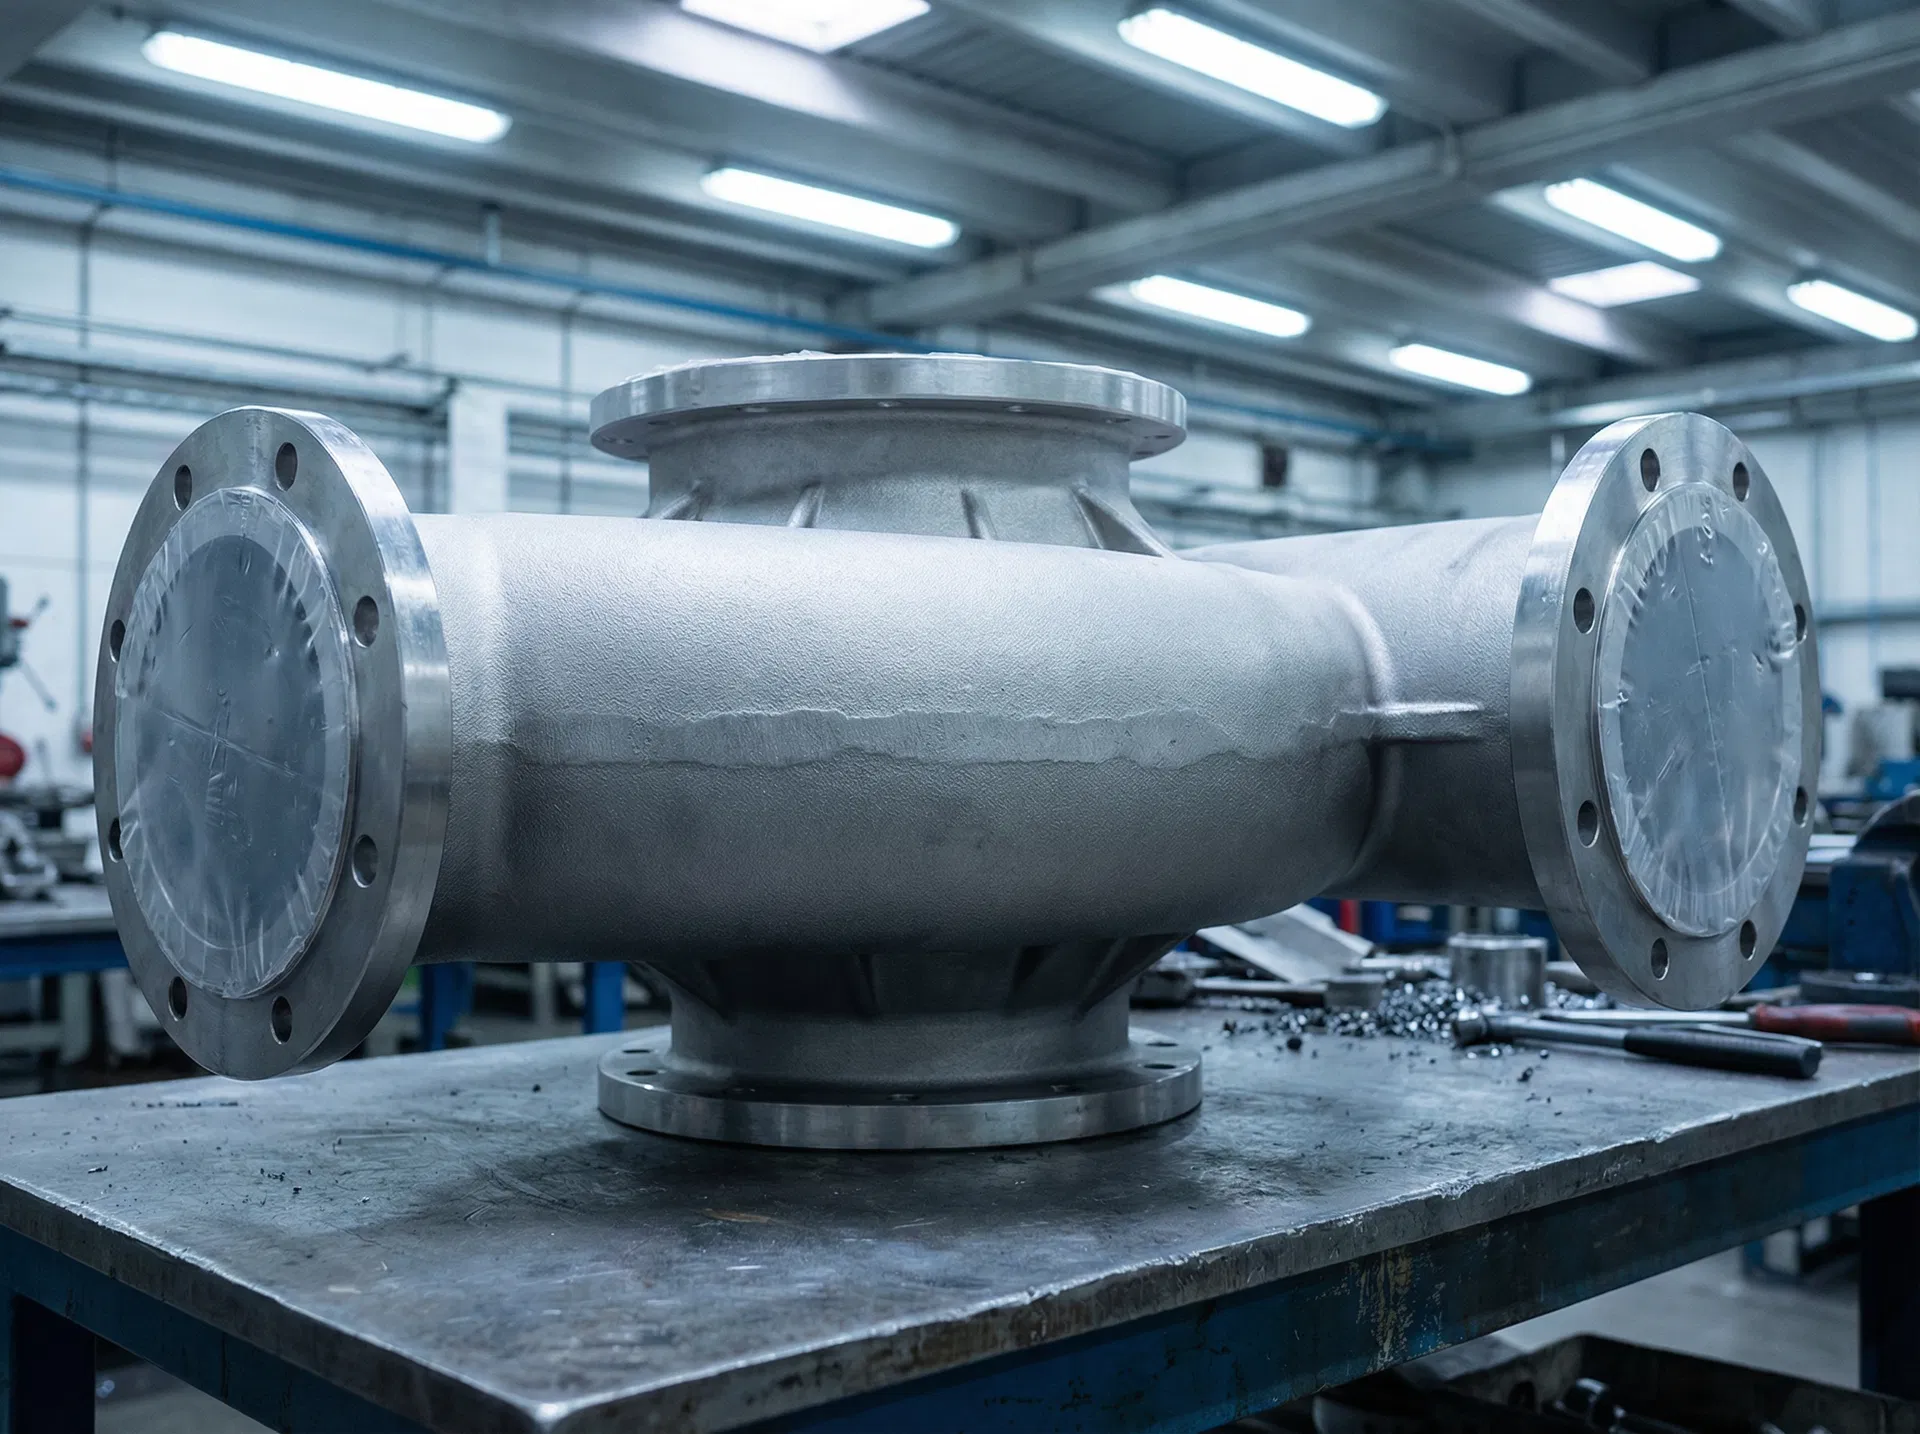
Pump Housings & Volute Casings
Pressure-rated to PN40. Hydrostatic test standard.
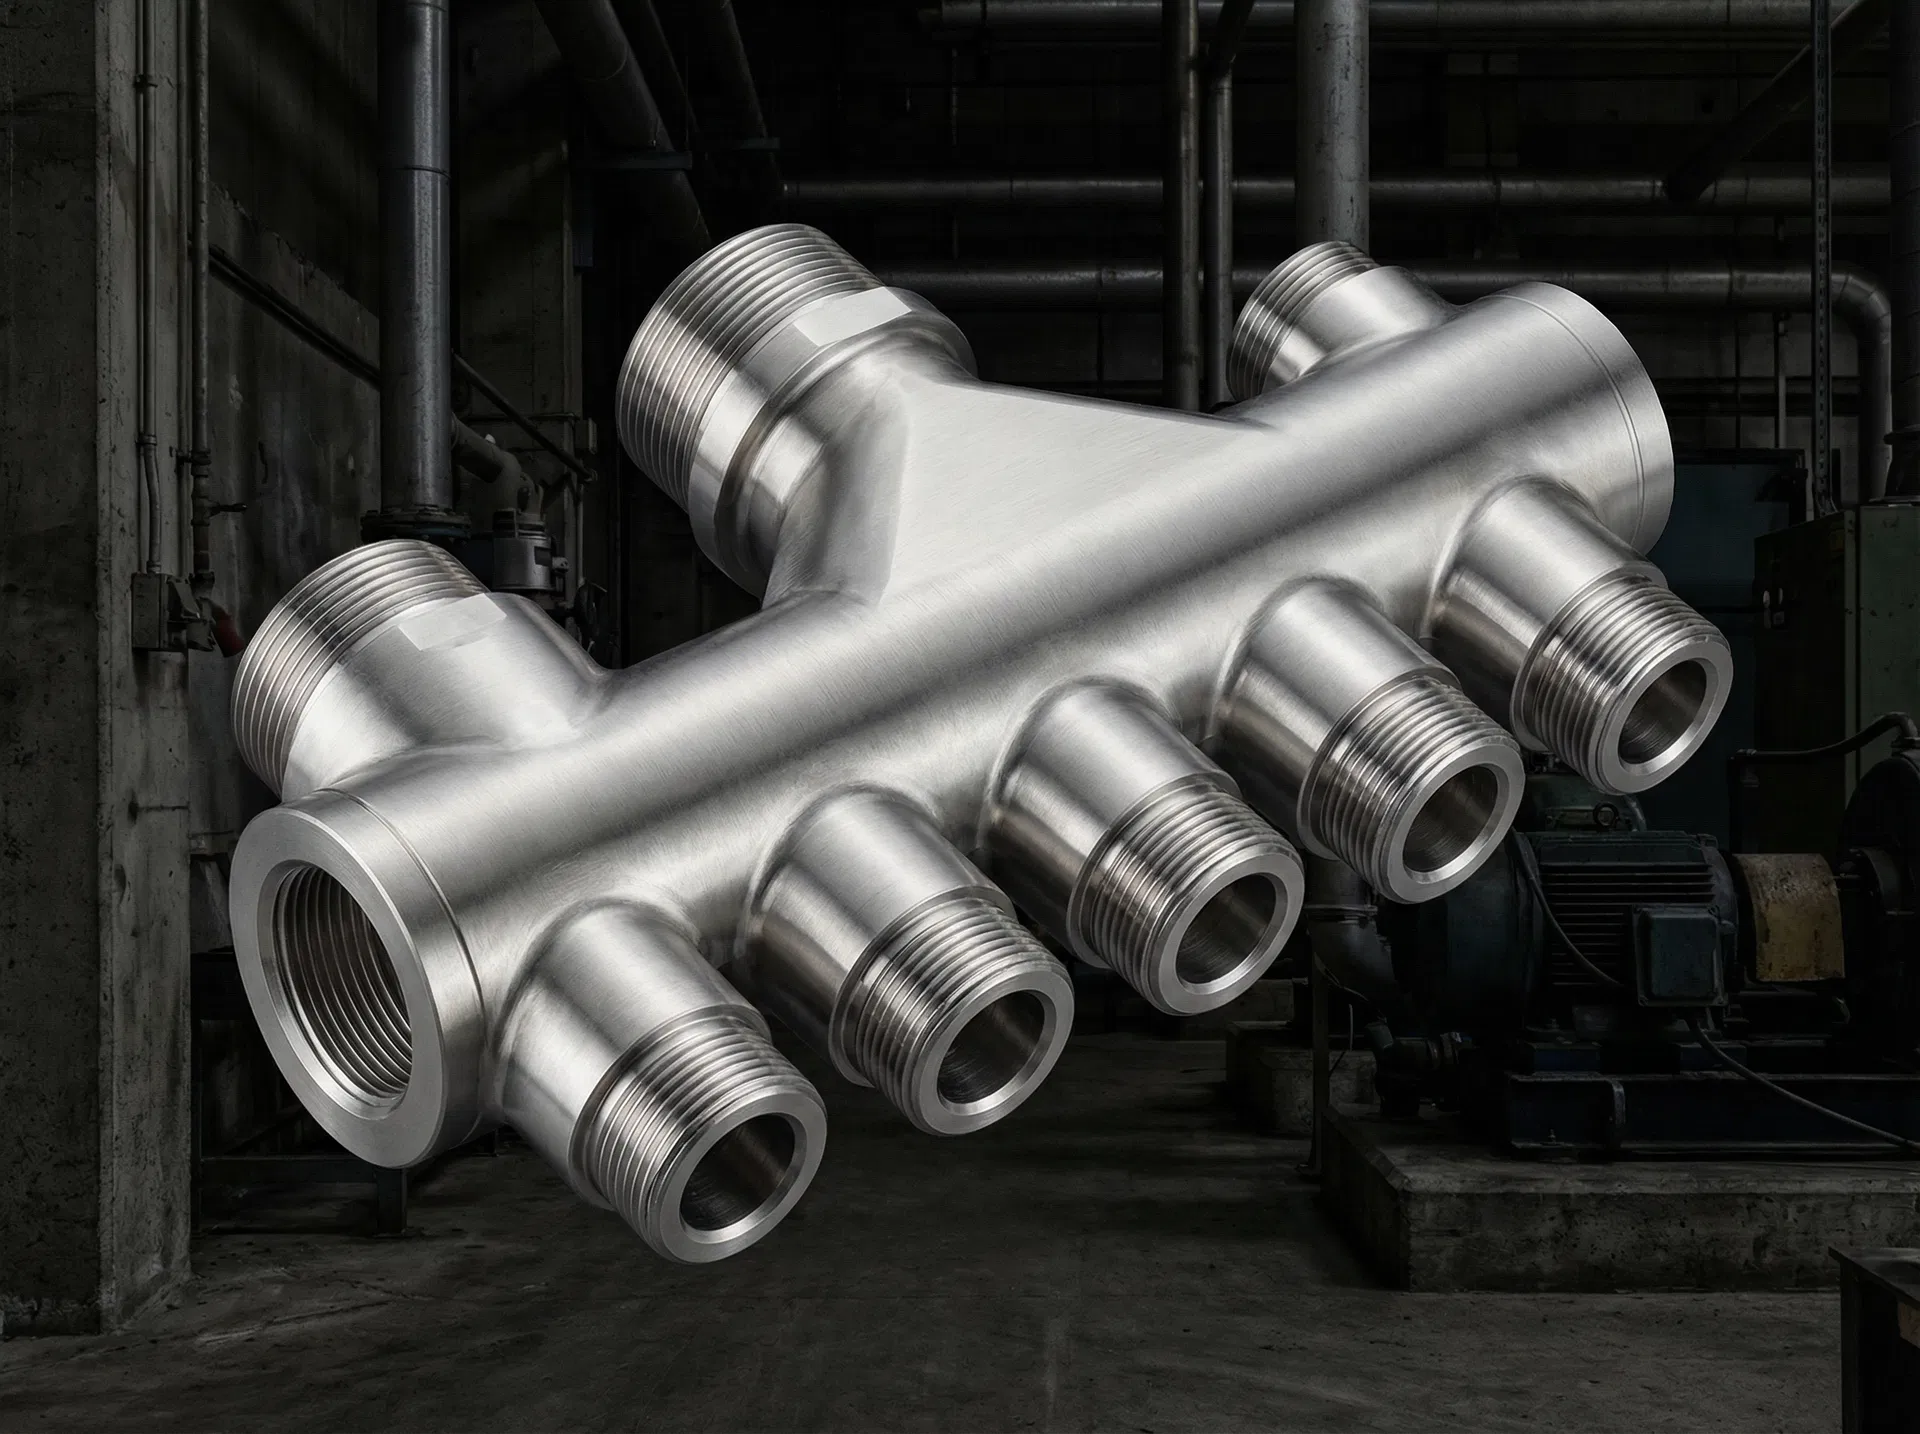
Manifolds & Multi-Port Bodies
Threaded, socket weld, butt weld available.
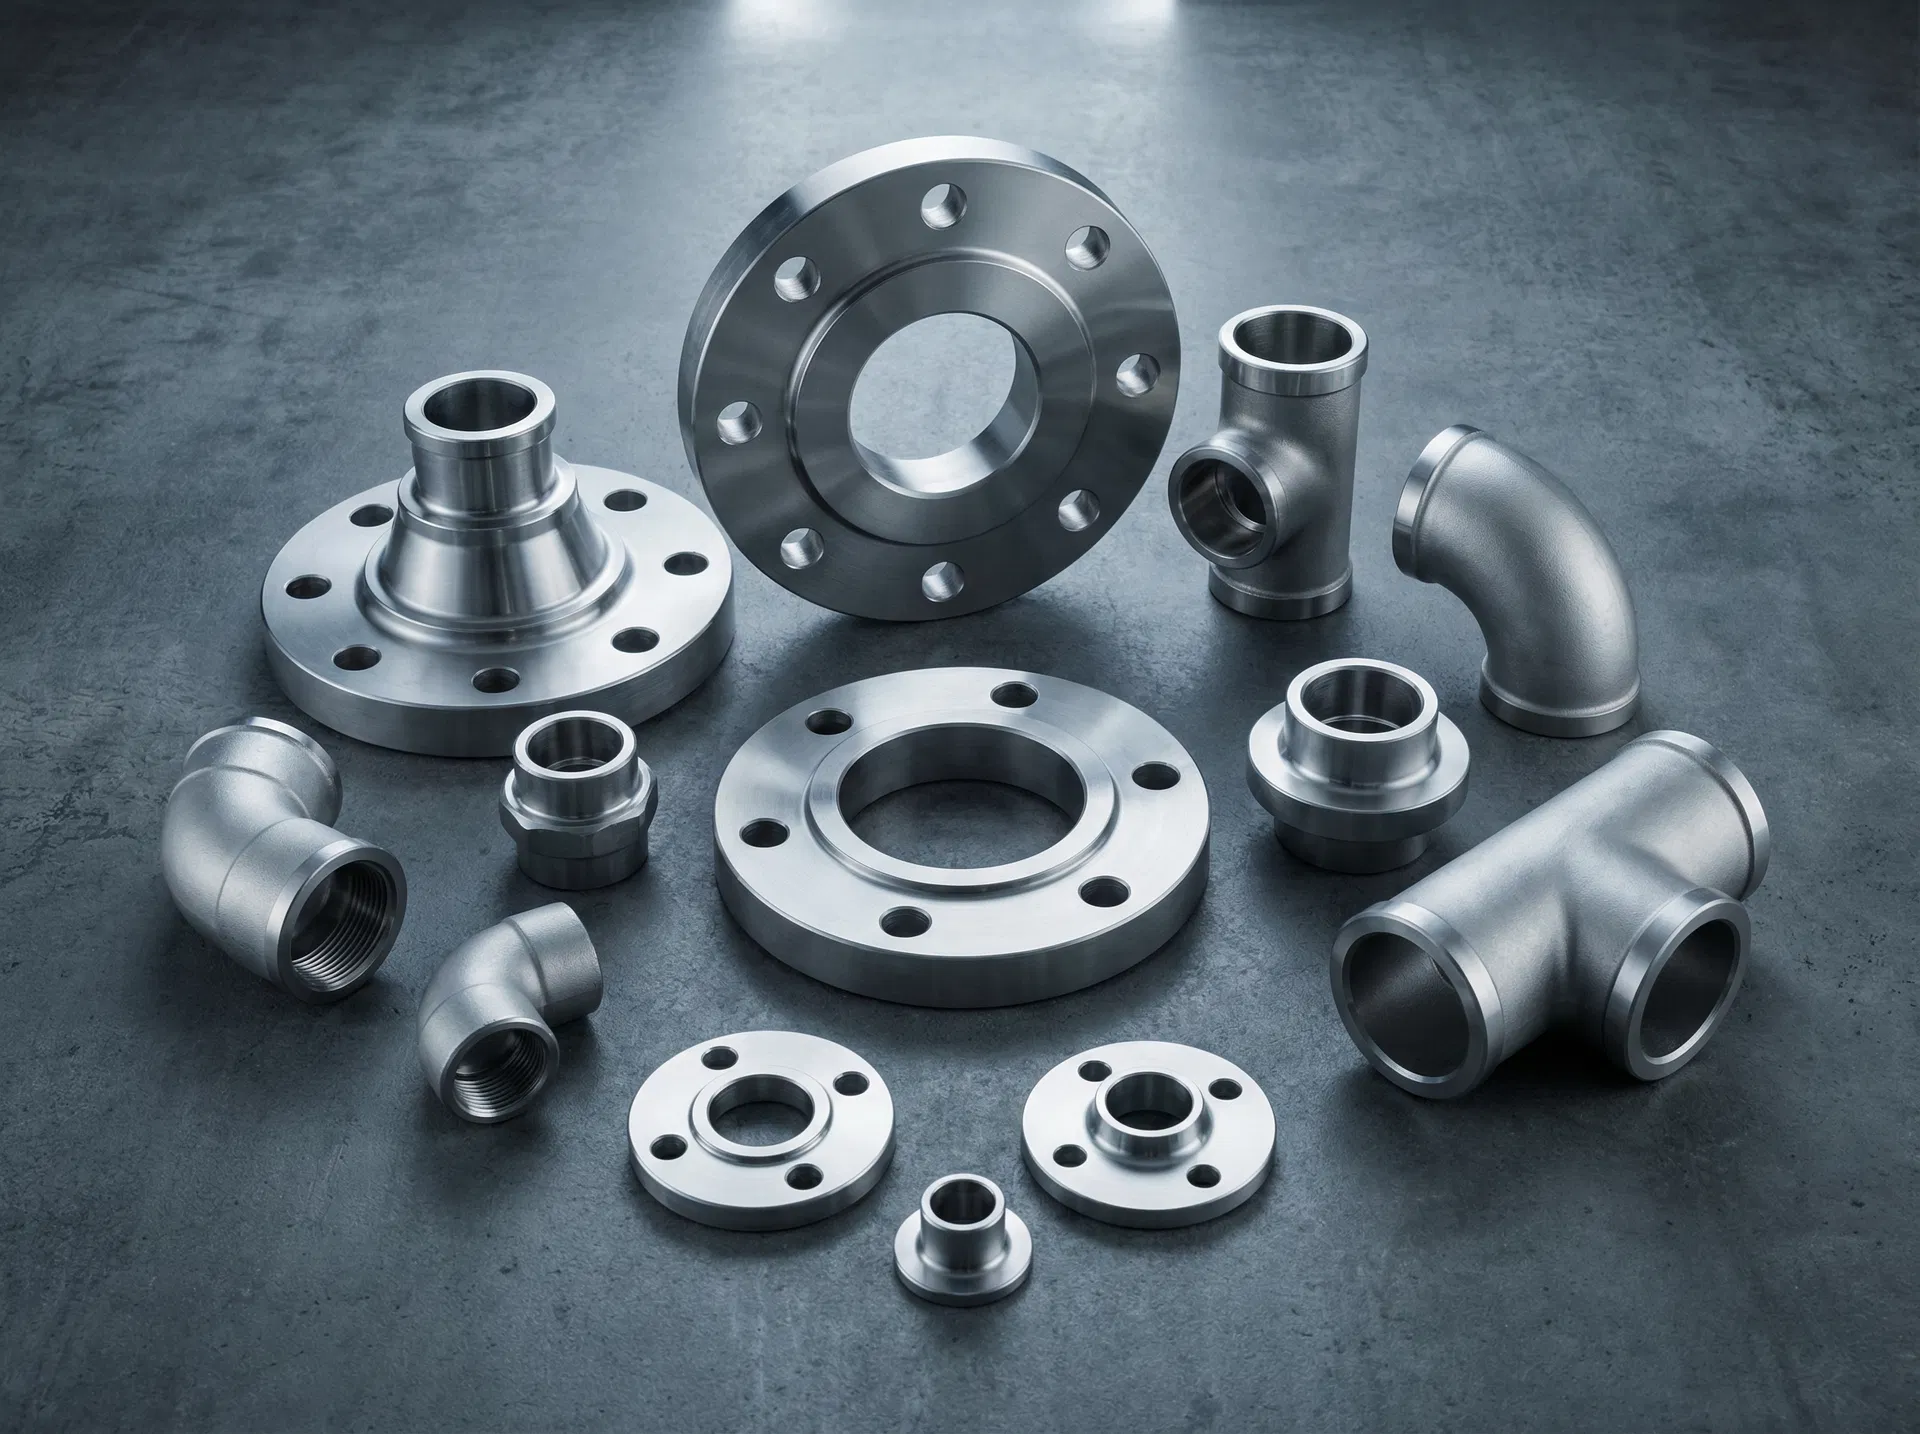
Flanges & High-Pressure Fittings
Raised face, flat face, ring-type joint available.
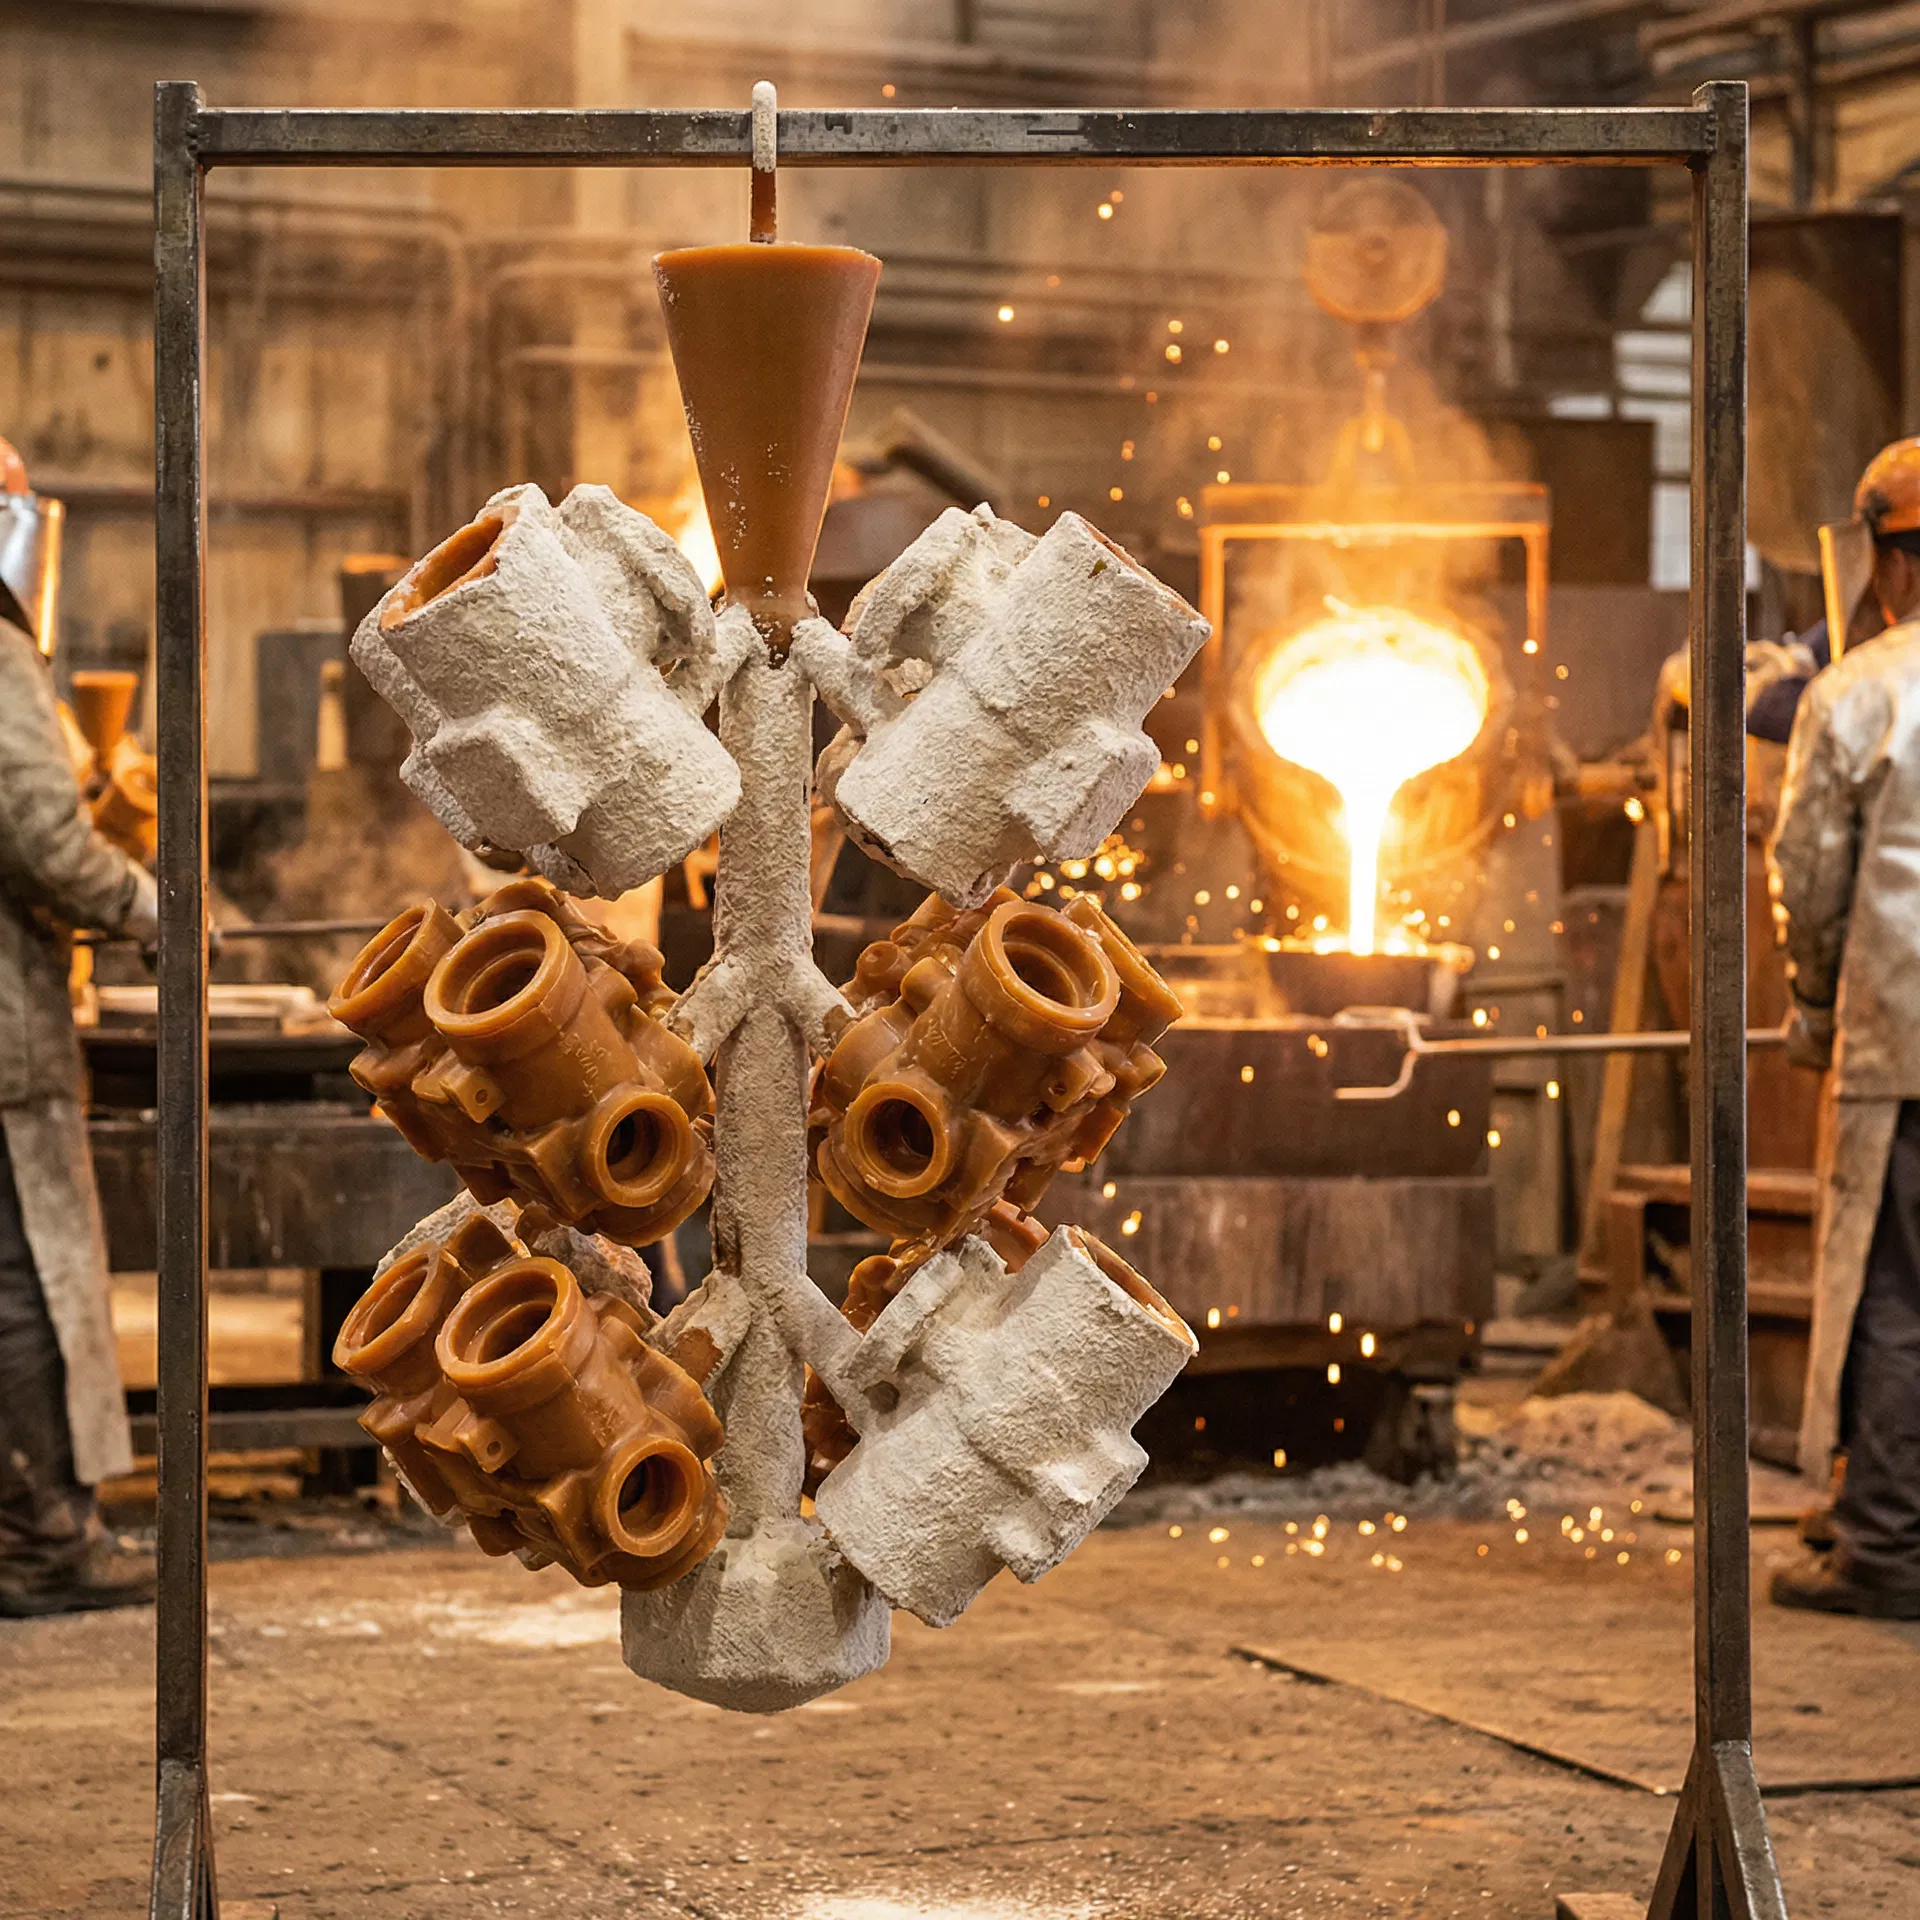
Wax Pattern Tree — Silica Sol Process
Real foundry. Not a trading company.
Real Foundry. Not a Trading Company.
Silica Sol Lost-Wax Investment Casting — From Wax Pattern to Finished Part
Every valve body and pump impeller starts with a precision wax pattern injected in our toolroom. The silica sol ceramic shell process ensures zero macro-porosity and consistent internal geometry — critical for pressure-tight applications.
Technical Data
Casting Specifications
| Casting Process | Silica Sol (Lost-Wax) Investment Casting |
| Weight Range | 0.05 kg – 50 kg per piece |
| Dimensional Tolerance | ISO 8062 CT4–CT6 (as-cast) |
| Surface Roughness | Ra 3.2–6.3 μm (as-cast); Ra 0.8–1.6 μm (machined) |
| Pressure Testing | 100% hydrostatic test for valve & pump parts |
| NDT Options | PT, UT, X-Ray, Magnetic Particle (on request) |
| Material Cert | EN 10204 3.1 Mill Test Certificate (standard) |
| Standards | ASTM A351, ASTM A743, EN 10213, API 6D |
| MOQ | 50 pcs (prototype: 5 pcs) |
| Lead Time | Tooling: 15–20 days | Production: 25–35 days |